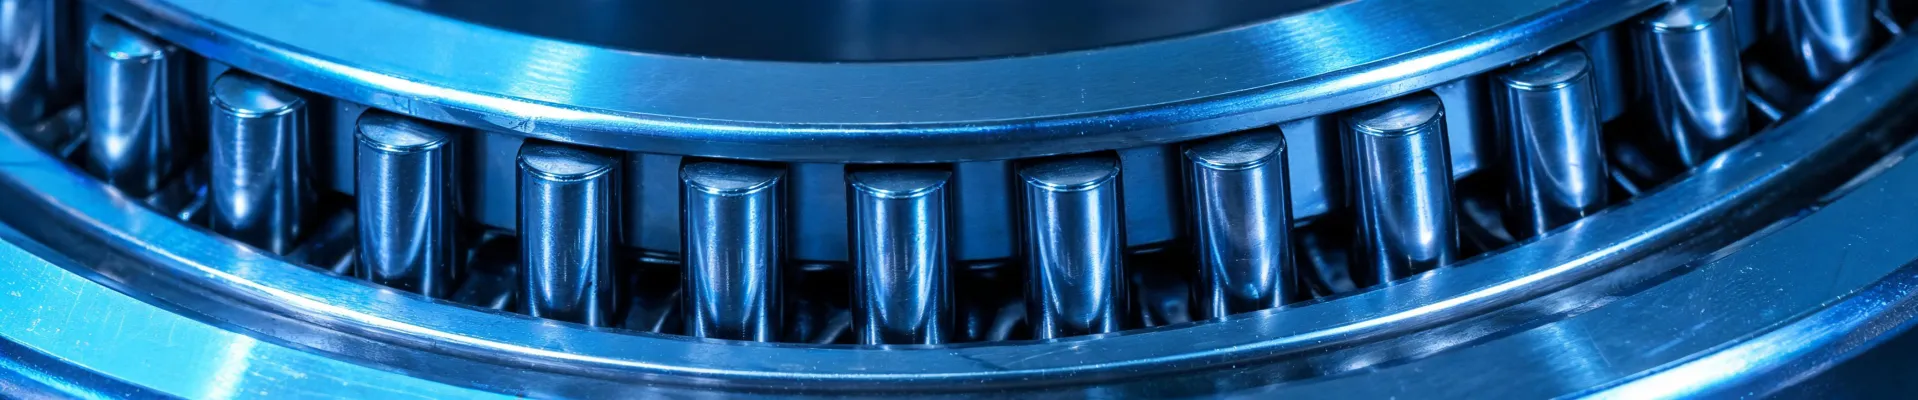
Before I get to the comparison, a confession: I caused the actuator failure. Not the vendor, not the operator, not bad parts. Me.
In 2017, I ordered 60 INA deep groove ball bearings for a new linear transfer unit. The bore matched. The load looked fine. I approved it. Two weeks into commissioning, one bearing seized, and by the end of the month, 14 were showing serious heat. We scrapped all 60. The cost was about $2,800 in bearings and three days of production downtime, not counting the embarrassment. That was my introduction to what happens when a linear actuator fails.
It took me four years and 13 field failures to understand that bearing selection isn't about picking a brand. It's about picking the right bearing geometry for the load path. INA, the Schaeffler Group brand, makes both needle roller bearings and deep groove ball bearings, and they are both excellent. They are also completely different animals.
The comparison that matters
The comparison that has caused me the most pain is not INA vs another brand. It's needle roller bearings vs deep groove ball bearings in the same machine. Both are useful. The difference is what they tolerate.
Look, I get why people default to a deep groove ball bearing. It's forgiving. Needle bearings are not. To be fair, a needle bearing does exactly what the catalog promises when the housing is rigid, the load is radial, and the alignment is true. But those three conditions don't happen by accident.
Dimension 1: radial capacity in a tight envelope
A needle roller bearing packs a lot of contact length into a small space. That's its entire personality. You can fit a needle bearing where a deep groove ball bearing with the same radial capacity wouldn't fit. For thin housings, gearboxes, and compact actuator cartridges, INA needle roller bearings make sense.
The word that carries the trap is 'pure.' A pure radial load is easy to calculate. Real radial loads come with side forces, bracket flex, thermal expansion, and the way the machine actually bolts together. In my experience, a needle bearing is the right answer when the radial envelope is the bottleneck and you have genuinely controlled the load path. If not, the capacity advantage disappears quickly.
Dimension 2: axial loads and surprise forces
A deep groove ball bearing handles radial and axial loads. A needle roller bearing, for the most part, doesn't. Some designs add a separate axial bearing, but a plain needle bearing shouldn't be asked to carry thrust.
Linear actuators are full of axial reactions. The lead screw pushes, the carriage pushes back, the motor mount flexes, the belt tension changes. If you support that shaft with a needle bearing selected for radial compactness, you're putting an axial load on a component that wasn't designed for it. In 2019, I watched it happen: belt-driven actuator, needle bearing at the output shaft, 30,000 cycles to failure. I changed it to a deep groove ball bearing, and it passed a 100,000-cycle test without issue. No other change. Same housing, same shaft, same load.
Dimension 3: misalignment tolerance—the one that bit me
Here's the thing: deep groove ball bearings tolerate a little angular misalignment. The balls sit in curved races, so a small tilt gets absorbed. Needle roller bearings don't work that way. The rollers are long and cylindrical; they need the raceways to stay parallel under load. Once they don't, the load concentrates at an edge, then the edge flakes, then the bearing jams.
The surprising part for me came in 2021. We had two identical actuator designs side by side. One used an INA needle roller bearing, the other an INA deep groove ball bearing. The static numbers favored the needle bearing. But the housing flexed 0.12 mm under full load, and that was enough to kill it. The needle design failed at 40,000 cycles. The deep groove design has now passed 120,000 cycles. If you plot the failure chart, it looks wrong. It isn't.
Part of the problem is how we read catalog ratings. The static load rating in ISO 76 is based on a permissible contact stress, not on a durability test in a flexing machine. It's a useful number, but it assumes the bearing is mounted in a rigid system. My housing wasn't.
What happens when a linear actuator fails?
Different bearings give you different warnings, and this is where the choice matters operationally.
A deep groove ball bearing usually fails loudly. There is noise, vibration, maybe temperature rise. You have time to schedule a replacement. That's worth real money.
A needle roller bearing often fails suddenly. One roller skews, the race spalls, and the actuator locks. If that's on a production line, the line stops when the bearing stops, not when you planned for maintenance.
In 2018, a seized needle bearing stopped a packaging line for 14 hours. The bearing itself cost less than $40. The downtime and repair cost more than $4,700. The lesson wasn't 'needle bearings are bad.' It was: don't let a non-serviceable bearing live in an application that can't tolerate a surprise stop.
Where INA pillow block bearings fit
I don't want you to walk away thinking the only options are needle and deep groove. INA also makes pillow block bearings, and they solve a different problem entirely.
A pillow block bearing is a mounted housing with a spherical insert. The spherical outer race lets the insert align itself to the shaft a little during installation. That makes it useful for long shafts, conveyors, fans, and welded frames where you can't line-bore a housing. If your actuator or drive shaft is supported by a frame rather than a precision-machined bore, a pillow block is often the most practical choice.
It's not a substitute for a needle bearing in a high-cycle, high-speed actuator. But it is a substitute for a deep groove bearing when the structure around the shaft is the weak link. The spherical alignment does what a rigid housing can't.
So which INA bearing should you choose?
If you ask me, the answer is 'it depends on the failure you're trying to avoid.' But to make that useful, here is the checklist I now use:
- Choose needle roller bearings when radial space is tight, the load is predominantly radial, and the housing is machined in one setup. Check alignment in the mounted state, not just in the drawing.
- Choose deep groove ball bearings when loads come from multiple directions, alignment is uncertain, or you want a failure warning before the actuator stops. This is my default for linear actuator supports.
- Choose pillow block bearings for long shafts, fabricated structures, or any place where a precision housing would be overkill. The self-aligning insert handles initial misalignment, and replacement is simple.
And don't start with bore size. Start with load path. Bore size is the last thing I check. In my first year, I started with bore size and got a $2,800 lesson. Now I start with the question: what is this bearing actually being asked to do?
An informed customer asks better questions. I'd rather spend 10 minutes explaining bearing geometry than replace an actuator on a weekend. Because when a linear actuator fails, it's rarely the bearing's fault. It's the application's fault. And the application is something we can control.
Elena Markovic
Elena Markovic is an independent industrial motor and drive systems analyst covering induction motors, servo motors, stepper motors, and variable-frequency drives. She examines IEC 60034-30-1 efficiency classes, IEC 61800-9-2 drive-system losses, speed-torque curves, duty cycles, thermal limits, and feedback compatibility across operating envelopes. Her evidence-led guides help OEM engineers and plant teams select efficient motion packages, plan integration, and reduce commissioning risk.